Caglar İnovasyon
CAGLAR İNOVASYON

Optimize deep-hole drilling. Stabilize production.

Improving tool geometry, chip evacuation and the entire process chain: Adem Çağlar’s personal project experience from his former employment at Mercedes-Benz.

  • Significantly higher tool output
  • Significantly improved process reliability
  • Unexpected tool breakage largely avoided
Discuss your project
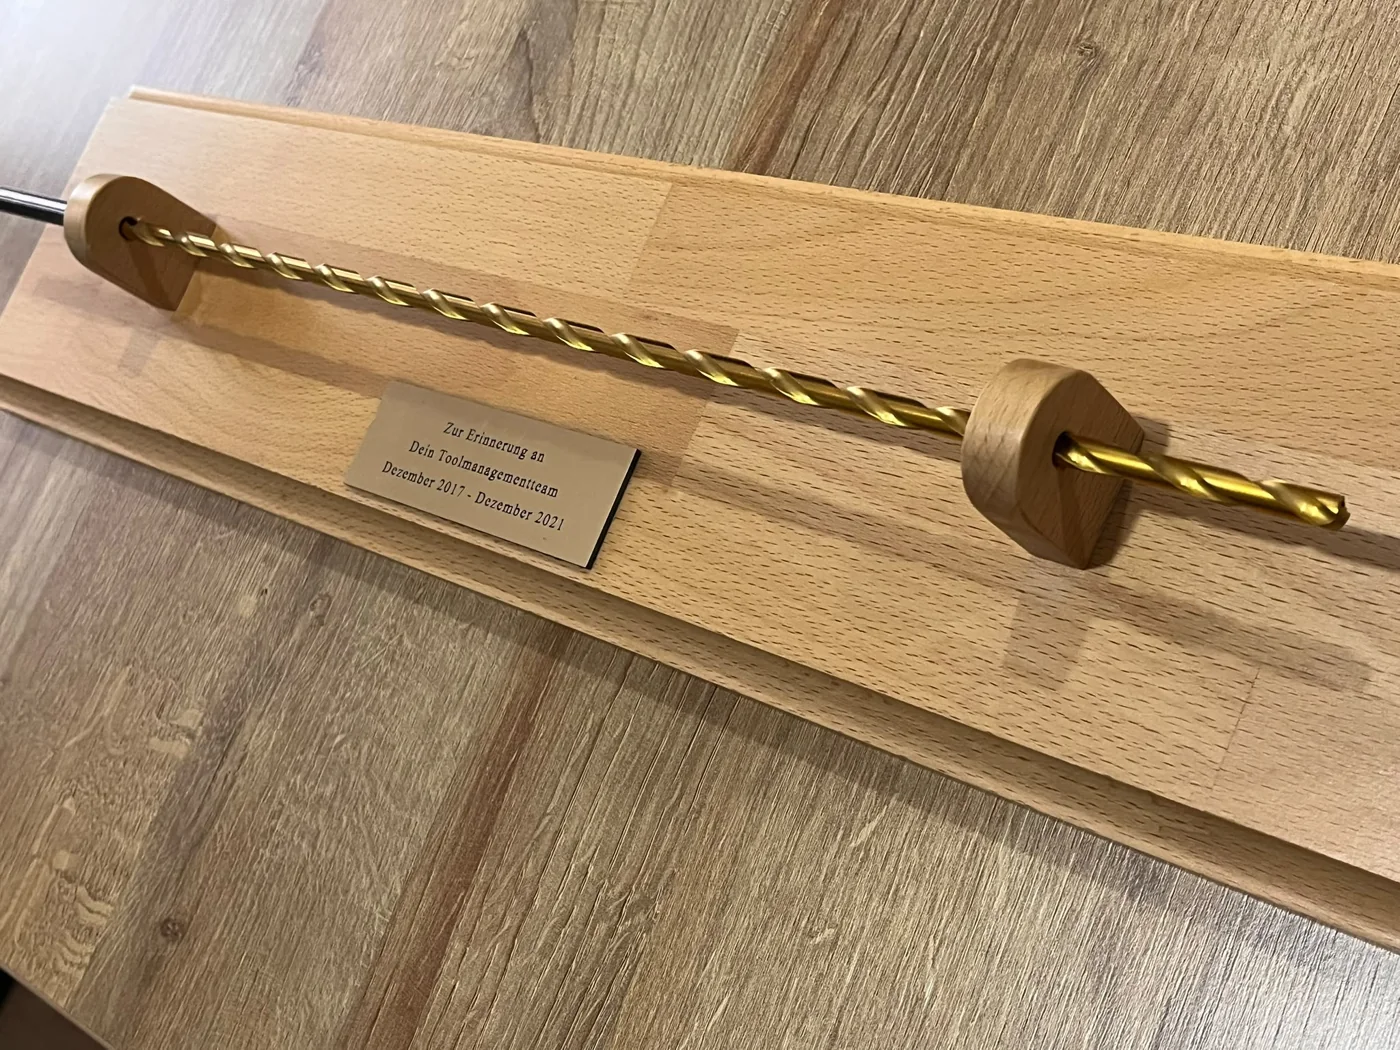
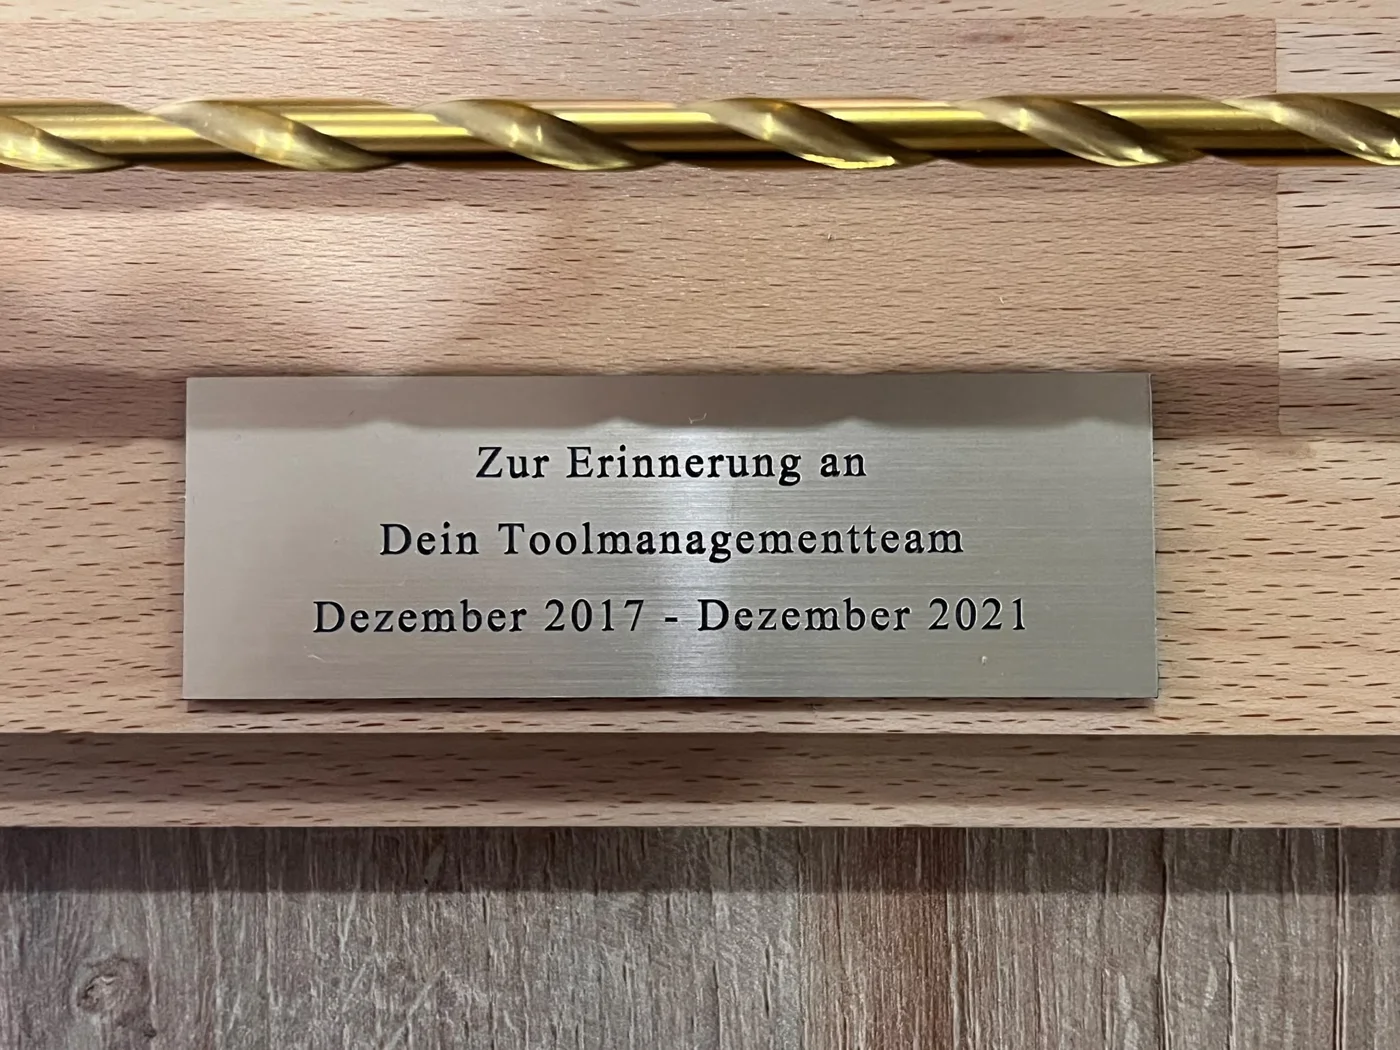
Original deep-hole drill · personal keepsake
PERSONAL INDUSTRIAL EXPERIENCE

Deep-hole drilling with MQL: stabilizing the entire process

A transmission shaft required demanding deep-hole drilling in series production. Recurring unexpected tool failures disrupted the process. The objective was higher average tool output and more reliable manufacturing.
Deep-hole drilling with MQL: stabilizing the entire process
Original deep-hole drill · detail of the keepsake

Tool output significantly increased – process reliability sustainably improved.

Before optimization

Recurring tool breakage · limited process reliability

After optimization

Significantly improved reliability · largely avoided unexpected breakage · more stable production
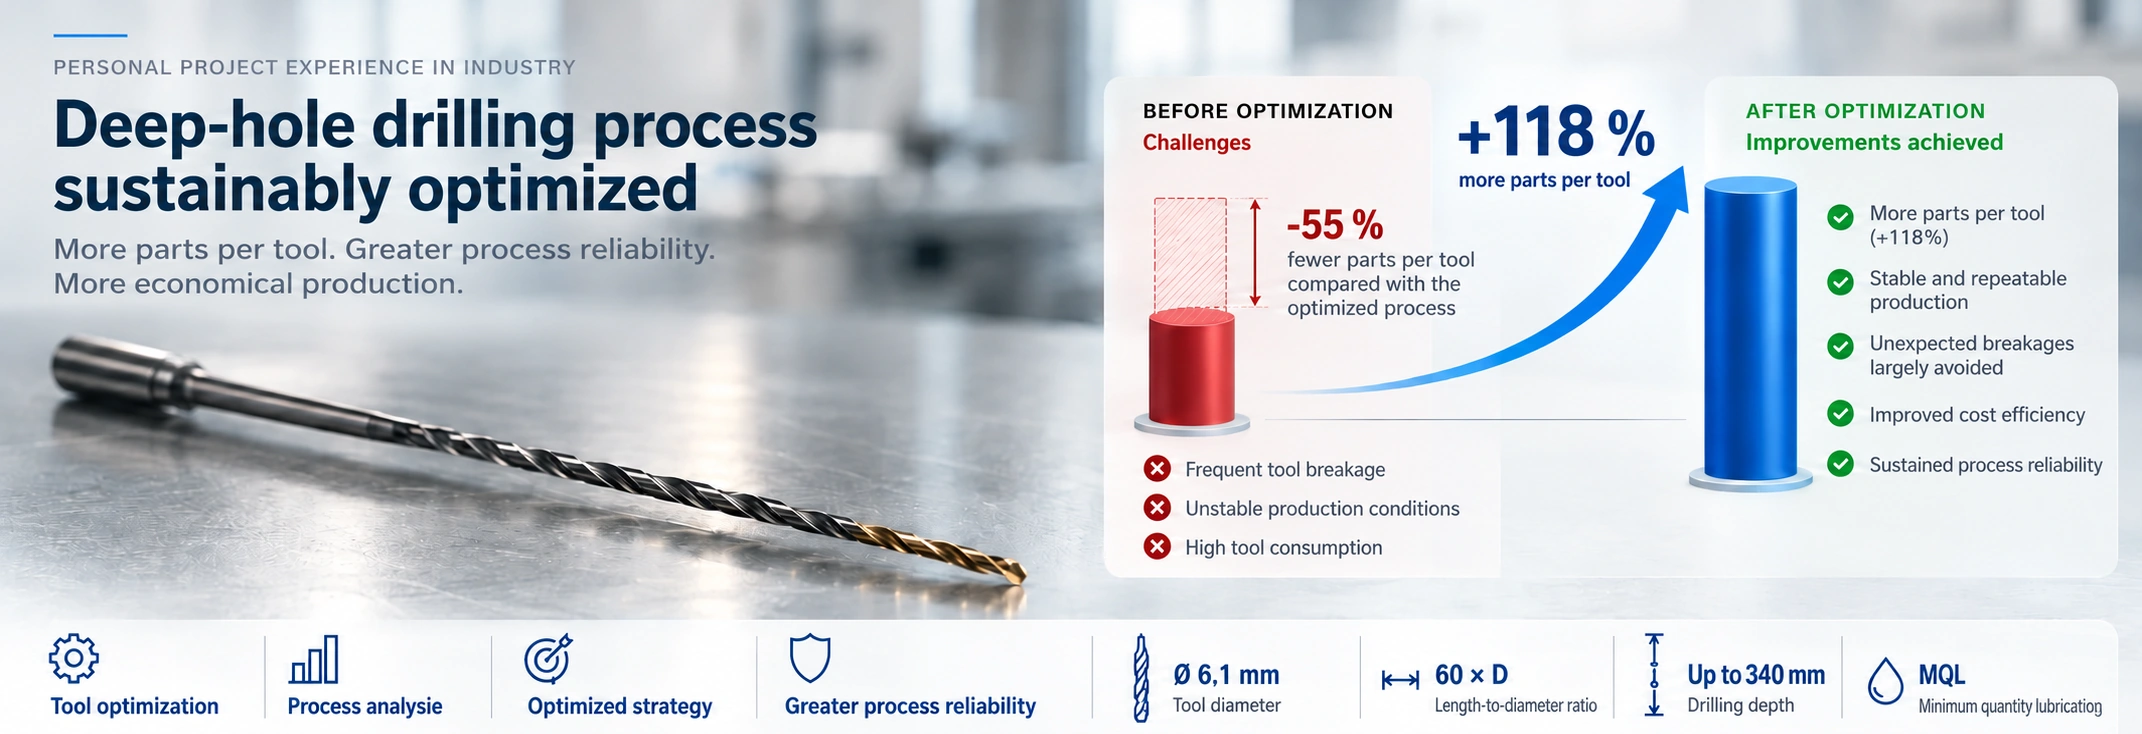
Project infographic · English version · schematic illustration, not an original photograph. Rounded percentages; the reference comparison is index 100 to 218.

Adem Çağlar worked on the optimization with colleagues, specialist departments and the tool supplier. The team examined the entire chain: supplier, presetting, storage, clamping, CNC program, production and shift operation.

  • Improve tool geometry, microgeometry, coating and regrinding
  • Review tool quality, preparation and handling
  • Coordinate CNC programs, drilling strategy, chip evacuation and MQL conditions
  • Standardize tool changes and process monitoring across shifts

Tool output significantly increased – process reliability sustainably improved.

Personal experience from former employment, not a Caglar İnovasyon customer project. Naming former employers does not imply a current business relationship or official endorsement. No third-party brand logos are added.

Adem Çağlar · Managing Director

Discuss your manufacturing process

Want to improve tool life, reduce breakage or stabilize production? Tell us about your process, bottleneck and objective.

Discuss your manufacturing process
Practical process improvement examples

50% less machining time

Adapted tool geometry halved machining time in a customer project.

Read the milling case

Diamond spring for cross-holes

A technical deburring application. Customer-specific savings have not yet been demonstrated.

Explore deburring
CAGLAR İNOVASYON · CUSTOMER CASE

Small change. Big impact.

Where others see limits, we discover new possibilities.

−50 %Machining time

Machining time comparison

Before · 100 %
After · 50 %

Optimized tool geometry. More economical manufacturing. New capacity.

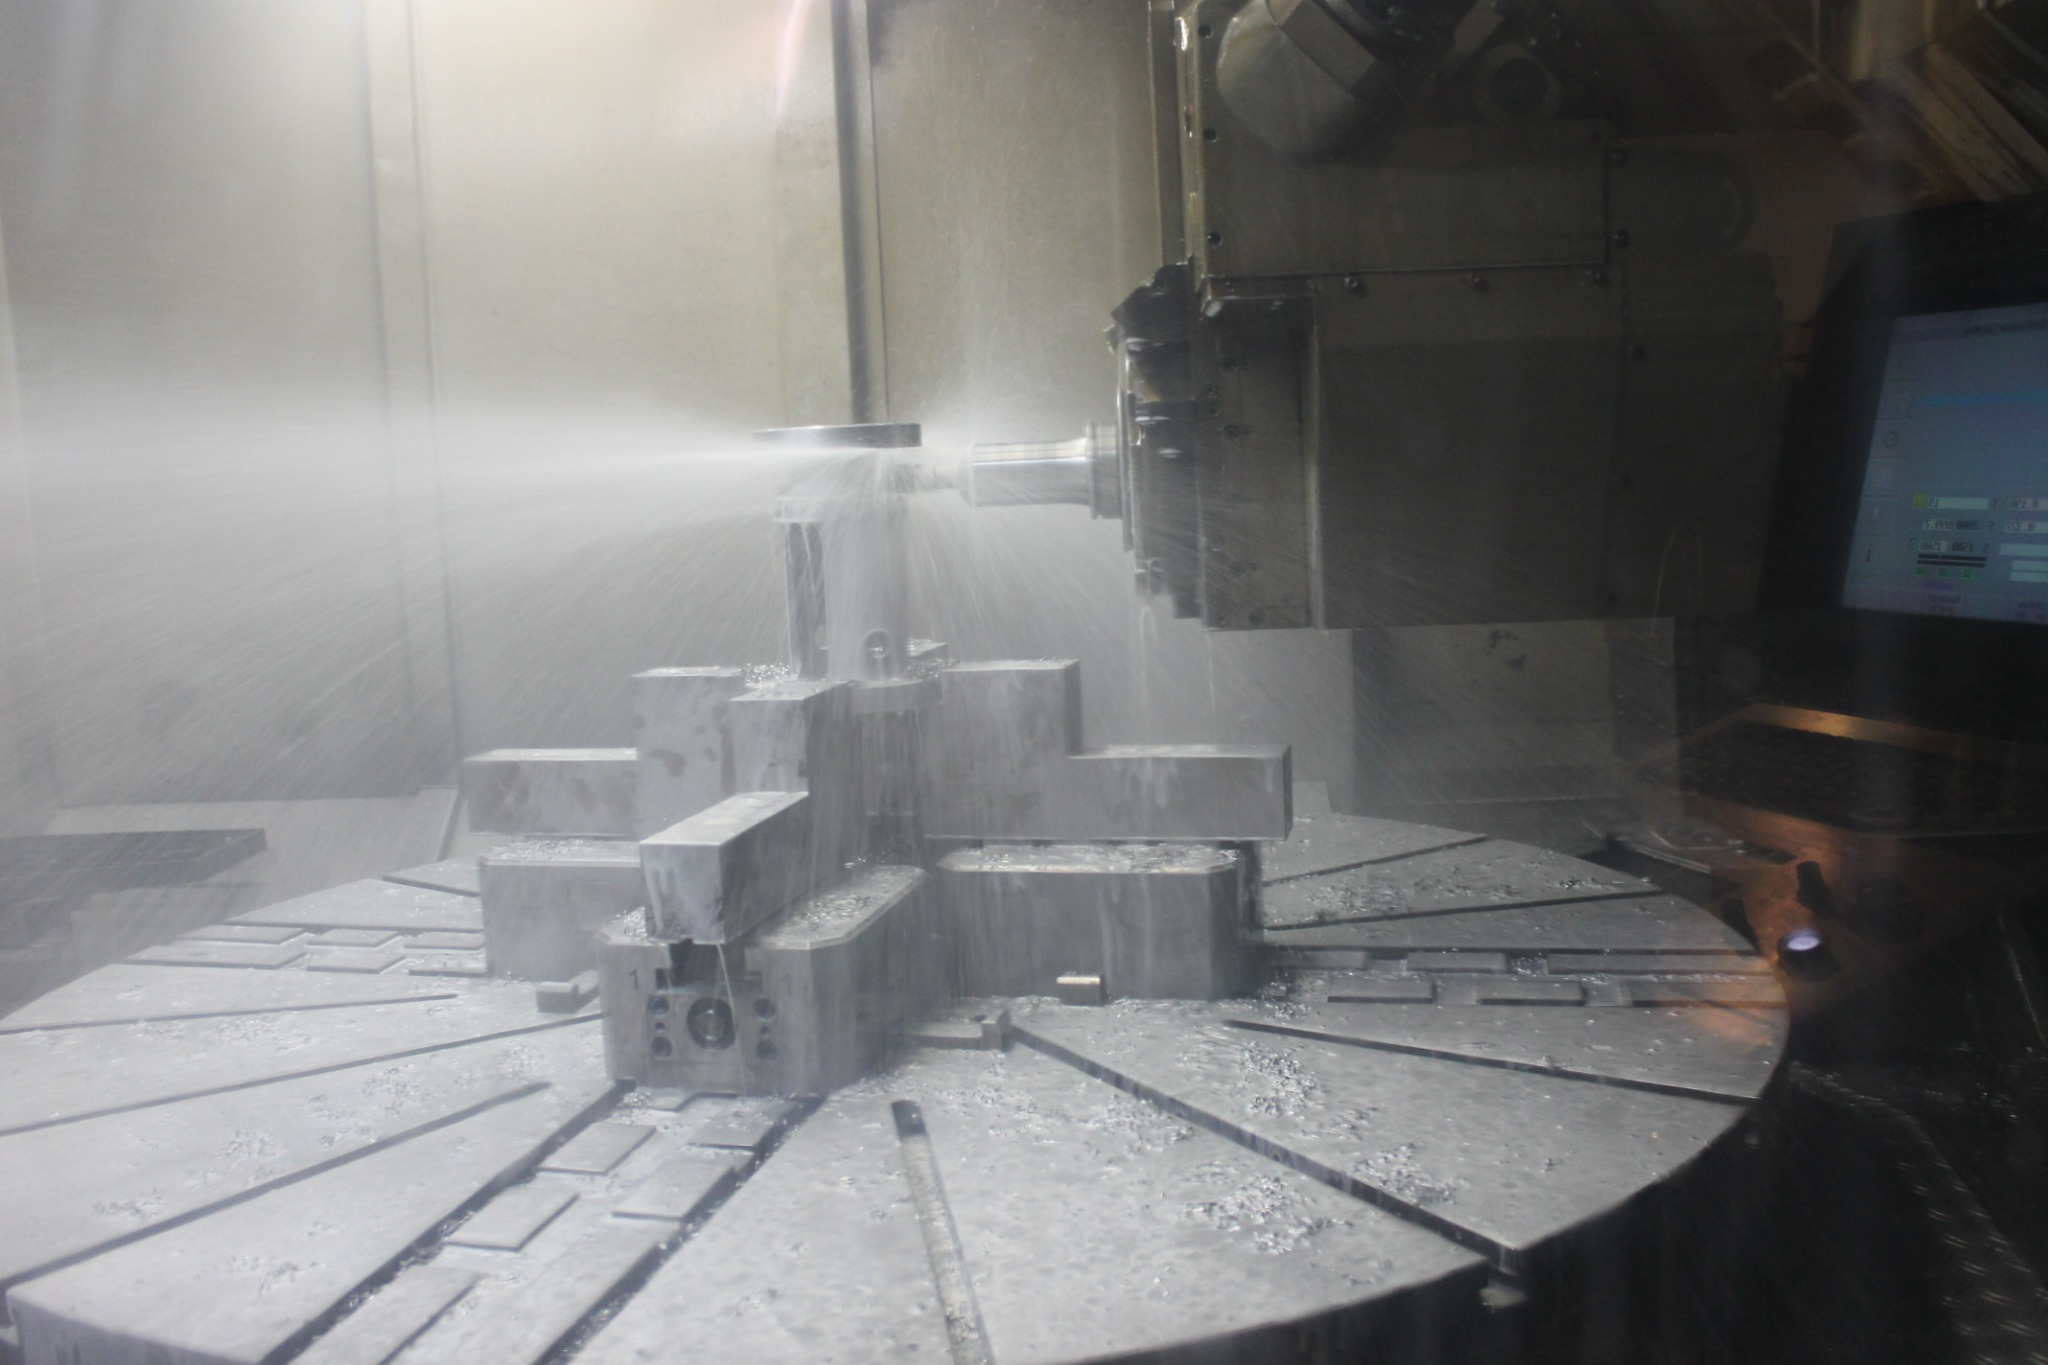
CNC machining with coolant
CNC machining with coolant. This photo illustrates the manufacturing environment; it does not show the specific before-and-after trial.
Selection of metal-cutting tools
Selection of metal-cutting tools. This photo provides context; it does not establish which exact tool was used in the customer trial.

A targeted change in tool geometry halved a customer’s machining time. A practical case of more competitive manufacturing and released machine capacity.

Explore the customer case
Original photograph · diamond spring deburring tool · click to enlarge
TASO · Diamond spring deburring tool

Targeted, economical deburring of cross-holes.

For hard-to-reach burrs at internal bore intersections: the flexible diamond spring tool supports controlled, repeatable deburring within the machining process.

Build process reliability

Match the tool, travel and machining parameters to the bore geometry and quality target.

Save time

Reduce manual rework and integrate deburring into the machining sequence.

Reduce cost per part

Optimise machining time, tool life and rework together.

The flexible spring geometry adapts to the surface. Suitability, edge quality and economics are evaluated on the actual component. Performance is not guaranteed for every geometry or material.

Discuss your deburring task
TASO · DIAMOND SPRING

How the diamond spring works

The animation shows internal cross-hole deburring during forward travel and withdrawal, with an enlarged detail view.

21 seconds · no audio · English labels

Principle animation, not footage of a physical trial. The values shown are an application example, not universal machining recommendations. Validate the tool, parameters and chip evacuation on the actual component.

Read the process steps
  1. The rotating tool enters the main bore axially. The illustrated entry chamfer is 3.5 mm long.
  2. During forward travel, burrs are removed from the cross-hole edges.
  3. The edges are deburred again during withdrawal; the direction of rotation remains unchanged.
  4. The animation illustrates chips being carried out during withdrawal. Complete chip evacuation must be verified in the actual process.
36+years of machining experience
20years at Mercedes-Benz
DE · TR · ENTechnical collaboration across borders

Experience that translates into machining practice.

Adem Çağlar brings over 36 years of machining experience and 20 years at Mercedes-Benz. His experience includes development work and process optimisation in tool management for transmission and engine production at Mercedes-Benz in Untertürkheim, CAD/CAM, and manufacturing projects in die and mould making at Mercedes-Benz. Today, Caglar İnovasyon supports companies with tool selection, machining strategies and economical manufacturing processes.

Supply references and professional experience

Supply references in Türkiye
BoschSelsaPolteks
Professional background · 20 years of employment
Mercedes-Benz

Mercedes-Benz is listed as part of Adem Çağlar’s employment history. This does not imply a supply relationship or endorsement of Caglar İnovasyon by Mercedes-Benz.

From bottleneck to measurable results

01 · Understand the process

Review the component, material, machine, tooling, cycle time and quality requirements together.

02 · Develop the solution

Align cutting parameters, tool geometry, tool life, workholding and deburring.

03 · Evaluate through trials

Compare the baseline and trial using quality, machining time and tool consumption under comparable conditions.

04 · Implement in production

Document validated parameters and support implementation with your manufacturing team.

Technical collaboration across borders

Analysis and technical coordination in German, Turkish and English. Remote support and on-site assignments by project agreement. Focus areas: drilling, milling, turning, deburring, tool management and minimum quantity lubrication.

Frequently asked questions

What is needed for an initial assessment?

Details of the operation, material, tool, cycle time, tool life and quality issue.

How is improvement measured?

Compare the baseline and trial under comparable conditions, considering cycle time, tooling cost, scrap and part quality together.

Do you guarantee a saving percentage?

No fixed saving is promised before investigation and trials. Targets are agreed for the individual project.

Technical Insights and Applications

All articles
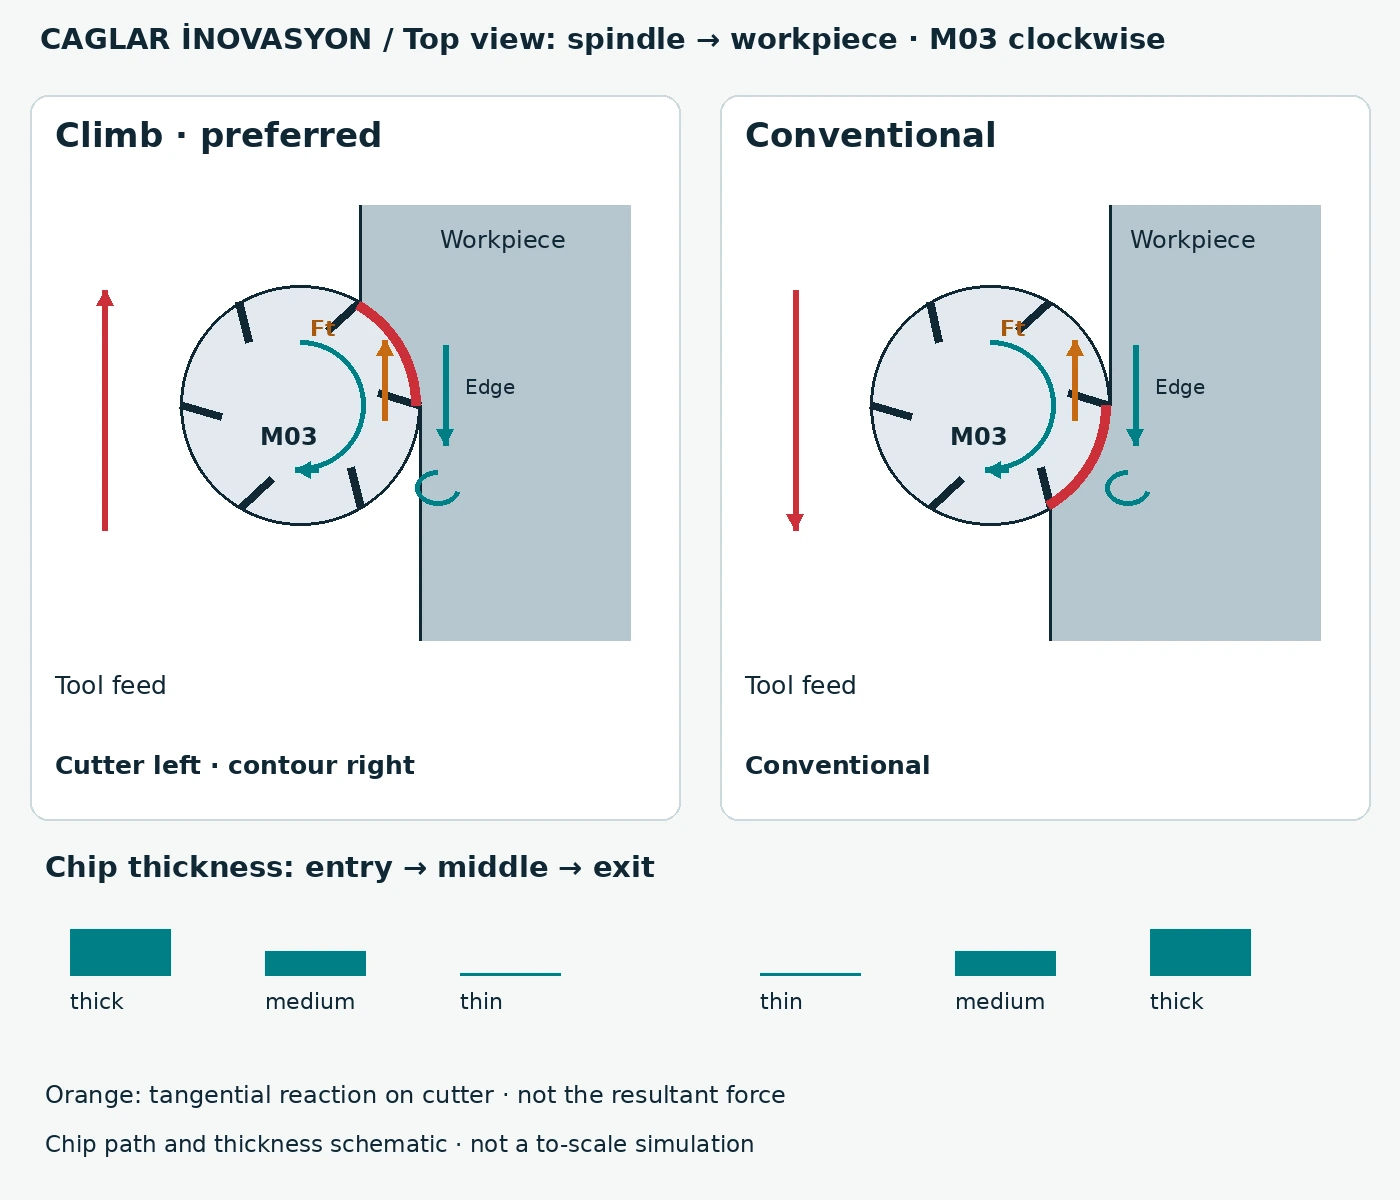
Top view from spindle towards workpiece. M03 clockwise. Red: tool feed; teal: edge motion; orange: tangential reaction on cutter. Original schematic.

Climb and conventional milling

Distinguish cutter rotation, workpiece feed and chip formation, then consider the machine before choosing the direction.

Outline your project

Start with your task and desired outcome. The appropriate scope is clarified in direct discussion.

Prepare a quotation enquiry

Cutting Data Calculator: milling, drilling and turning

Calculate spindle speed, cutting speed, feed, material removal rate and theoretical machining time. Free, no registration, entirely in your browser.

Cutting Data Calculator: milling, drilling and turning
ALPMILL F1